Compliance requires more information than product name
Clip machine and consumable compatibility; The closing movement of the machine is controlled by examining the clip sizes it accepts and the feeding pattern of the roll. The definition of “double wire roll” or “single wire clip” alone is not sufficient. For compatibility, the technical requirements of the model must match the measured description of the consumable.
Two rolls of the same length may have different wire diameter, tape width or winding structure. Just because someone physically settles into the machine does not prove that it will feed properly and produce the desired seal. Consumable replacement should be considered together with the packaging sample.
This check is not done only when buying a new machine. It is also necessary to re-examine the previous matching when the supplied consumables change, a new packaging is switched or the dimensions of the current application are updated.
Save pattern and closing motion
Write the brand/model information of the machine on the nameplate or product document. If there are different configurations of the same model, indicate this. The label of the current consumable and a photograph of the closed packaging help explain the binding action.
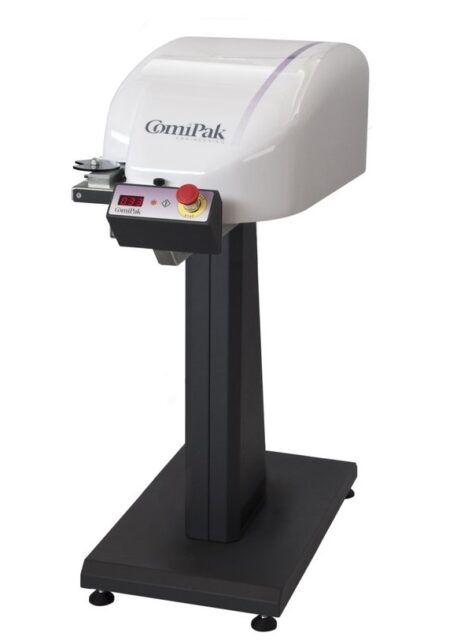
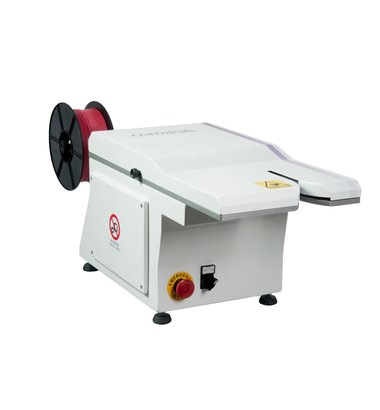
Single-wire binding and tape-clip closure are different systems. For example 104TW with single wire binding applications, M-408PL It is evaluated together with tape clip applications. This distinction narrows the family of consumables; does not constitute an endorsement of a particular roll.
Instead of trying vague settings to adapt the machine to the consumption, rely on the model’s operating instructions and authorized technical evaluation. Covers, guards or safety devices should not be modified to ensure product compatibility.
Prepare comparison chart for roll and clip
| Information | What does it clarify? | How to share? |
|---|---|---|
| wire structure | Single-wire or double-wire consumable family | Product name and close-up |
| bandwidth | Feed and shut-off geometry | Measurement in millimeters |
| wire diameter | Technical structure of the consumable | Product description or technical drawing |
| Cutting length | Pieces used per package | Model and application requirement |
| Roll dimensions | Placement on carrier and feed | Core, external dimensions and winding information |
| Winding direction | How the consumable enters the machine | Photo showing direction |
| Roll length | Consumable quantity and replacement plan | Quantity per meter and roll |
Which dimensions are critical may vary depending on the model. Do not guess for an unknown value; Clarify based on existing consumables or technical documentation. Measurement guideexplains the distinction between wire diameter and total covered size.
Evaluate the way packaging arrives at the machine
The mouth of the bag coming into the machine, the filling amount and the product height are part of the trial. Collecting the section to be closed differently each time will change the results, even if the consumption is correct. Therefore, evaluation made with only empty bags may not represent the full package flow in its entirety.
In systems using horizontal or vertical placement, product support and operator movement are also important. GPV40 IND In models evaluated with different layouts, such as bag size, how the product is carried should also be described. A photo of the production area can facilitate layout negotiation.
Compare consumable replacement to a controlled trial
First record the closure accepted with the current consumable for reference. Then evaluate the new consumable in the same packaging and conditions. Authorized personnel must perform the operation and adjustment of the machine in accordance with the model’s instructions.
- Write the current consumable code and the new candidate’s code.
- Record packaging material, filling and closing dimensions.
- Observe feeding, cutting and closed product appearance separately.
- Note the number of downtime, rework, and unusable parts.
- Keep the confirmed conditions for the next order.
Do not change more than one variable at a time during the experiment. If both the packaging, the roll and the working order change, it becomes difficult to separate the cause of the result. When a recurring problem occurs, instead of intervening in the cutter or feeding system, transfer the observation to the technical team with model information.
Interpret speed and meter information correctly
The cycle interval specified by the manufacturer does not mean that the entire line will operate at the same speed. The movements of taking, placing, closing and removing the bag affect the total time. Roll changes and assortment changeovers should also be included in the daily capacity.
Roll length shows the amount of consumption; Does not indicate machine capacity. To calculate the theoretical number of parts roll clip consumption account use it. Plan purchase quantity by comparing results with actual wastage and operating records.